AWS A5.9 ER308L
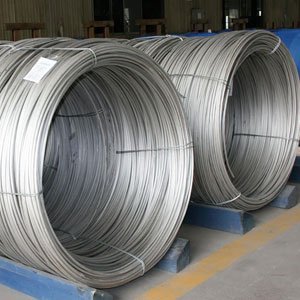
ER308L Filler Wire
19.5–22.0% Cr / 9.0–11.0% Ni low-carbon (0.03% max C) wire for 304 and 304L stainless steel piping, cryogenic tanks and food machinery.
Comprehensive range of austenitic, low-carbon, stabilized, high-silicon, martensitic, ferritic and super-austenitic stainless steel welding filler wires exported from India.
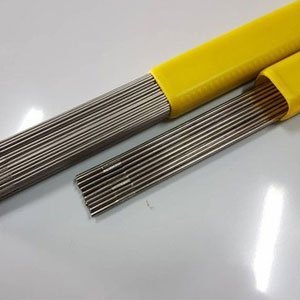
FillerWires supplies a full metallurgical spectrum of bare stainless steel welding wires and cut-length rods manufactured in accordance with AWS A5.9 / ASME SFA-5.9 and EN ISO 14343. Whether fabricating hygienic 304L food processing tanks, chloride-resistant 316L offshore piping, dissimilar carbon-to-stainless vessel nozzles with 309L, or 310 refractory furnace internals, our stainless filler wires provide controlled delta-ferrite balance, low residual tramp elements (P, S) and clean arc transfer.
Contact us for confirmed product specifications and available technical documentation.
19.5–22.0% Cr / 9.0–11.0% Ni low-carbon (0.03% max C) wire for 304 and 304L stainless steel piping, cryogenic tanks and food machinery.

18.0–20.0% Cr / 11.0–14.0% Ni / 2.0–3.0% Mo low-carbon wire for marine, pharmaceutical and chemical process 316/316L fabrication.
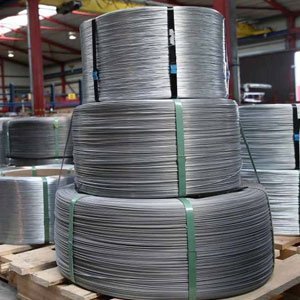
23.0–25.0% Cr / 12.0–14.0% Ni over-alloyed low-carbon wire for dissimilar stainless-to-carbon steel joints and first-layer cladding.
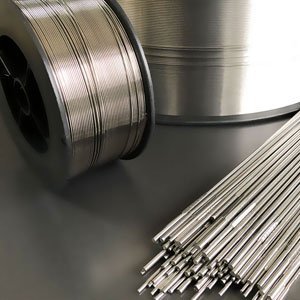
25.0–28.0% Cr / 20.0–22.5% Ni fully austenitic wire for high-temperature furnace parts, radiant tubes and heat-resisting castings.
In addition to our four primary stainless grades above, FillerWires supplies the following specialized austenitic, super-austenitic, martensitic and ferritic grades:
Ultra-low carbon 18Cr-8Ni filler wire for general 304/304L stainless steel fabrication and nitric acid equipment.
Controlled carbon (0.04–0.08% C) 19Cr-9Ni filler wire for elevated-temperature creep resistance in 304H catalyst and refinery piping.
Silicon-enriched (0.65–1.00% Si) low-carbon 308L wire for improved weld pool wetting and smooth bead toe profile in GMAW/MIG.
High-silicon 24Cr-13Ni low-carbon wire for high-speed GMAW dissimilar joining and smooth stainless overlay cladding.
23Cr-13Ni-2.5Mo filler wire for buffer layers under 316L cladding on carbon steel and dissimilar welding of molybdenum-bearing steels.
Low-carbon 25Cr-22Ni-2Mo fully austenitic wire engineered specifically for urea strippers and severe carbamate service.
Modified high-chromium nickel austenitic wire for specialized high-temperature and chemical process welding.
Work-hardening Mn-bearing austenitic filler wire for armor plate, Austenitic manganese steel (Hadfield) and hard-to-weld steels.
High-ferrite (~29Cr-9Ni) crack-resistant filler metal for extreme dissimilar steel combinations, tool steels and maintenance repair.
Silicon-enhanced (0.65–1.00% Si) 18Cr-12Ni-2.5Mo wire delivering superior arc stability and wetting in MIG and TIG applications.
Higher molybdenum (3.0–4.0% Mo) low-carbon filler wire for severe chloride pitting and flue-gas desulfurization service.
Niobium-stabilized Cr-Ni-Mo filler wire for welding stabilized Ti/Nb 316Ti and 316Cb stainless steels at elevated temperatures.
Low-residual Nb-stabilized Ni-Cr-Mo-Cu wire for welding Carpenter Alloy 20 in sulfuric acid service (see Alloy 20 page).
Niobium (Columbium) stabilized 19Cr-9Ni filler wire preventing intergranular carbide precipitation in 321 and 347 stainless steels.
27Cr-31Ni-3.7Mo-1Cu super-austenitic filler metal (Alloy 28 type) for wet-process phosphoric and sulfuric acid heat exchangers.
20Cr-25Ni-4.5Mo-1.5Cu super-austenitic filler wire for welding 904L stainless steel in chloride, sulfuric and phosphoric acid plants.
Fully austenitic low-carbon Cu/Mo-alloyed wire resistant to crevice corrosion, stress-corrosion cracking and seawater cooling duty.
12% Cr martensitic stainless steel wire for valve seats, hydroturbine runners and 410/403 base metals (requires preheat & PWHT).
12Cr-4.5Ni-0.5Mo low-carbon martensitic wire with improved toughness and cavitation resistance for CA6NM castings and hydro turbines.
16% Cr ferritic stainless steel filler wire for automotive exhausts, nitric acid drums and thermal-expansion-matched overlays.
Reference comparison of AWS A5.9 wire chemistry limits across key stainless steel filler metal classifications. Contact us for confirmed product specifications and available technical documentation.
| AWS Grade | UNS No. | C | Cr | Ni | Mo | Mn | Si | Other Elements | Primary Welding Application |
|---|---|---|---|---|---|---|---|---|---|
| ER308L | S30883 | 0.03 | 19.5–22.0 | 9.0–11.0 | 0.75 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | AISI 304 / 304L vessels, piping & cryogenic service |
| ER308LSi | S30888 | 0.03 | 19.5–22.0 | 9.0–11.0 | 0.75 | 1.0–2.5 | 0.65–1.00 | Cu 0.75 | High-speed GMAW (MIG) of 304/304L with improved wetting |
| ER309L | S30983 | 0.03 | 23.0–25.0 | 12.0–14.0 | 0.75 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | Dissimilar carbon-to-stainless joints & barrier cladding |
| ER309LMo | S30986 | 0.03 | 23.0–25.0 | 12.0–14.0 | 2.0–3.0 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | Dissimilar joints & buffer layers beneath 316L overlays |
| ER310 | S31080 | 0.08–0.15 | 25.0–28.0 | 20.0–22.5 | 0.75 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | AISI 310 furnace parts & scaling resistance to 1150°C |
| ER312 | S31380 | 0.15 | 28.0–32.0 | 8.0–10.5 | 0.75 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | High-ferrite dissimilar steel & maintenance welding |
| ER316L | S31683 | 0.03 | 18.0–20.0 | 11.0–14.0 | 2.0–3.0 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | AISI 316 / 316L chemical, marine & pharmaceutical piping |
| ER317L | S31783 | 0.03 | 18.5–20.5 | 13.0–15.0 | 3.0–4.0 | 1.0–2.5 | 0.30–0.65 | Cu 0.75 | AISI 317L severe pitting & flue-gas desulfurization |
| ER347 | S34780 | 0.08 | 19.0–21.5 | 9.0–11.0 | 0.75 | 1.0–2.5 | 0.30–0.65 | Nb+Ta: 10×C–1.0 | Stabilized AISI 321 & 347 refinery service (425–850°C) |
| ER385 (904L) | N08904 | 0.025 | 19.5–21.5 | 24.0–26.0 | 4.2–5.2 | 1.0–2.5 | 0.50 | Cu 1.2–2.0 | 904L sulfuric/phosphoric acid & seawater equipment |
| ER410NiMo | S41086 | 0.06 | 11.0–12.5 | 4.0–5.0 | 0.40–0.70 | 0.60 | 0.50 | Fe Bal. | CA6NM hydro-turbine runners, pump castings & valves |
FillerWires welcomes B2B enquiries for AWS A5.9 stainless steel TIG rods and MIG spooled wires from industrial buyers across the following target countries and cities:
| Target Country | Relevant Industrial Cities & Ports | Primary Stainless Grades Requested |
|---|---|---|
| United Arab Emirates (UAE) | Dubai, Abu Dhabi, Sharjah, Jebel Ali, Ras Al Khaimah, Fujairah | ER316L, ER308L, ER309L, ER316LSi |
| Oman | Muscat, Sohar, Duqm, Salalah, Sur | ER316L, ER309L, ER347, ER317L |
| Saudi Arabia | Dammam, Jubail, Riyadh, Jeddah, Yanbu, Khobar | ER309L, ER310, ER316L, ER347, ER385 (904L) |
| Qatar, Kuwait & Bahrain | Doha, Ras Laffan, Mesaieed, Kuwait City, Ahmadi, Manama, Hidd | ER308L, ER316L, ER310, ER309LMo |
| United States & United Kingdom | Houston, Pittsburgh, Chicago, Los Angeles, Aberdeen, Sheffield, Birmingham | AWS A5.9 ER308L, ER316L, ER309L, ER347, ER410NiMo |
| Italy, Germany & Netherlands | Milan, Turin, Genoa, Bologna, Hamburg, Düsseldorf, Rotterdam, Eindhoven | EN ISO 14343 / AWS A5.9 ER316L, ER316LSi, ER308LSi, ER385 |
| Singapore, Sri Lanka, South Africa & Peru | Jurong, Tuas, Colombo, Trincomalee, Johannesburg, Durban, Lima, Callao | ER316L, ER308L, ER309L, ER312, ER904L |
Key metallurgical and procurement answers for AWS A5.9 / EN ISO 14343 stainless steel welding consumables.
Under AWS A5.9, ER308L (19Cr-9Ni, ≤0.03% C) is used for welding 304 and 304L stainless steels; ER316L (18Cr-12Ni-2.5Mo, ≤0.03% C) adds molybdenum for chloride pitting resistance in 316/316L equipment; ER309L (24Cr-13Ni, ≤0.03% C) is over-alloyed for dissimilar carbon-to-stainless steel welding and barrier cladding; and ER310 (25Cr-20Ni) is a fully austenitic wire for high-temperature oxidation resistance up to 1150°C.
Silicon-enriched grades (0.65–1.00% Si) improve molten weld pool fluidity, arc stability and toe wetting during semi-automatic and robotic GMAW (MIG) welding, reducing crown convexity and post-weld grinding.
FillerWires supplies AWS A5.9 stainless steel consumables as straight cut-length TIG rods (1.2mm to 4.0mm × 914mm / 1000mm in 5 kg / 10 kg tubes) and precision layer-wound MIG spools (0.8mm to 1.6mm on 12.5 kg / 15 kg BS300 spools).