Stainless Steel ER309L Filler Wire Supplier — AWS A5.9 ER309L Dissimilar Welding Wire
Over-alloyed 24Cr-13Ni low-carbon (0.03% max C) stainless steel filler wire (AWS A5.9 ER309L / UNS S30983) engineered for dissimilar metal welding between stainless steel and carbon or low-alloy steels and first-layer cladding.
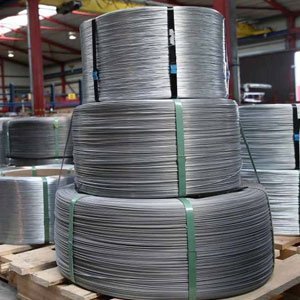
24Cr-13Ni Low-Carbon Filler Metal Built to Absorb Carbon Steel Dilution Safely
Stainless Steel ER309L Filler Wire (classified under AWS A5.9 ER309L and EN ISO 14343-A 23 12 L) is the industry-standard filler metal for dissimilar metal welding (DMW) between austenitic stainless steels (such as 304L, 316L, 321, 347) and carbon steels or low-alloy steels, as well as for depositing the first barrier layer of corrosion-resistant stainless weld overlay cladding onto carbon steel pressure vessels.
If a standard 18Cr-8Ni filler wire (like ER308L) were used to weld carbon steel to stainless steel, dilution with the unalloyed carbon steel (~25–35% dilution) would drop the weld metal chromium and nickel into the brittle martensitic zone on the Schaeffler/WRC-1992 diagram, causing cold cracking. ER309L solves this by over-alloying with 23.0–25.0% Chromium and 12.0–14.0% Nickel, ensuring that even after 30% carbon steel dilution, the resulting weld deposit retains a ductile, crack-resistant 18Cr-8Ni austenitic-ferritic microstructure.
Alloy Identification, Standards & Supply Specifications
Extra-low carbon (≤0.03% C) minimizes carbon pick-up and carbide precipitation along the ferritic-to-austenitic fusion boundary.
| Product Designation | Stainless Steel ER309L Filler Wire (TIG Welding Rod / MIG Spooled Wire) |
|---|---|
| AWS / ASME Classification | AWS A5.9 / ASME SFA-5.9 ER309L |
| EN / ISO Classification | EN ISO 14343-A W/G 23 12 L (W.Nr. 1.4332) |
| UNS Designation & Werkstoff Nr. | UNS S30983 • W.Nr. 1.4332 |
| Compatible Base Materials | Dissimilar joints between AISI 304 / 304L / 316 / 316L / 321 / 347 stainless steels and carbon/low-alloy steels (ASTM A516 Gr.70, A106 Gr.B, A36, A387); joining clad steel plates; and welding wrought/cast 309S / 309Cb base metals. |
| Supported Welding Processes | GTAW (TIG), GMAW (MIG), SAW |
| Shielding Gas Recommendations | 100% Argon (GTAW); Ar + 1–2% O2 or Ar + 2% CO2 (GMAW) |
| Available Wire Diameters | MIG Spools: 0.8mm (.030"), 0.9mm (.035"), 1.0mm (.040"), 1.2mm (.045"), 1.6mm (1/16") TIG Cut-Length Rods: 1.2mm, 1.6mm (1/16"), 2.0mm, 2.4mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32") × 914mm (36") / 1000mm |
| Packaging & Storage | TIG Rods: 5 kg / 10 kg moisture-resistant tubular plastic packs in export master cartons. MIG Wire: 12.5 kg / 15 kg precision layer-wound BS300 / S200 spools sealed in VCI polyethylene film. Storage: Store in a dry, temperature-controlled indoor store (+10°C to +40°C, <60% RH) in original sealed packaging. |
Chemical Composition Specification (AWS A5.9 / ASME SFA-5.9 ER309L)
The table below specifies the standard wire chemical composition limits in weight percent (wt.%). Single values represent maximum permissible limits unless stated otherwise:
| Element | Verified Specification Limit (wt.%) | Metallurgical Function in Weld Metal |
|---|---|---|
| Carbon (C) | 0.03 max | Low carbon suppresses martensite hardness and carbide sensitization at the fusion line |
| Chromium (Cr) | 23.0 – 25.0 | High chromium compensates for iron dilution when welding carbon/low-alloy steel |
| Nickel (Ni) | 12.0 – 14.0 | High nickel maintains austenitic stability despite base metal dilution |
| Manganese (Mn) | 1.0 – 2.5 | Deoxidation and solidification crack resistance |
| Silicon (Si) | 0.30 – 0.65 (ER309LSi: 0.65–1.00) | Weld puddle fluidity and toe wetting |
| Molybdenum (Mo) | 0.75 max (ER309LMo: 2.0–3.0) | Residual limit in ER309L (alloyed in ER309LMo) |
| Copper (Cu) | 0.75 max | Residual limit |
| Phosphorus (P) & Sulfur (S) | P ≤ 0.030, S ≤ 0.030 | Strict impurity control |
| Iron (Fe) | Remainder | Matrix balance |
Mechanical & Physical Properties
The values below distinguish between minimum AWS/ISO classification requirements for all-weld-metal test assemblies and typical as-welded deposited weld metal benchmarks:
| Property | Value | Unit | Specification / Reference Basis |
|---|---|---|---|
| Tensile Strength | ≥ 550 (Typical: 580 – 630) | MPa | Typical All-Weld-Metal Deposit (AWS A5.9 / ISO 14343) |
| Yield Strength (0.2% Offset) | ≥ 370 (Typical: 410 – 450) | MPa | Typical As-Welded GTAW/GMAW Deposit |
| Elongation | ≥ 30 (Typical: 34 – 38) | % | In 5D / 50 mm Gauge Length |
| Ferrite Number (FN) | 8 – 16 (Undiluted) | FN | Drops to ~4–10 FN after 25–30% carbon steel dilution |
| Density | 7.90 | g/cm³ | Physical Property Reference |
Corrosion Resistance, Welding Considerations & Industrial Applications
When welding carbon steel to stainless steel with ER309L, control arc placement and heat input to keep carbon steel dilution below 30%. Note: If the dissimilar joint will operate continuously above 315–425°C or undergo high-temperature Post-Weld Heat Treatment (PWHT), specify Inconel 82 (ERNiCr-3) or Inconel 625 (ERNiCrMo-3) instead of ER309L to avoid carbon migration and thermal expansion fatigue.
Typical Industrial Applications
- Welding carbon steel pipe supports, structural clips, skirts and saddles onto 304L/316L stainless steel pressure vessels
- First-layer barrier weld overlay cladding on carbon steel reactor shells and heat exchanger tubesheets (prior to ER308L or ER316L cap layers)
- Joining the stainless-clad side of roll-bonded or explosion-bonded clad pressure vessel plates
- Fabricating AISI 309 / 309S furnace baffles, boiler tube hangers and kiln liners
International Enquiry Destinations
FillerWires welcomes B2B export enquiries for Stainless Steel ER309L Filler Wire from EPC contractors, process equipment fabricators, shipyards and distributors across the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Typical Regional Sector Demand |
|---|---|---|
| United Arab Emirates & Saudi Arabia | Abu Dhabi, Dubai, Jebel Ali, Sharjah, Dammam, Jubail, Yanbu, Riyadh | Pressure vessel fabrication, clad columns & structural attachment welds |
| Oman, Qatar, Kuwait & Bahrain | Sohar, Muscat, Duqm, Doha, Ras Laffan, Ahmadi, Shuaiba, Manama | Refinery vessels, heat exchangers & process skids |
| United States & United Kingdom | Houston, Tulsa, Pittsburgh, Chicago, Sheffield, Birmingham, Aberdeen | ASME Section VIII vessel shops & petrochemical plants |
| Italy, Germany & Europe | Milan, Bergamo/Brescia, Turin, Genoa, Hamburg, Essen, Rotterdam | Clad heat exchangers, boilers & heavy fabrication |
| Singapore, Sri Lanka, South Africa & Peru | Jurong, Tuas, Colombo, Johannesburg, Durban, Lima, Callao | Process vessels, mining tanks & marine fabrication |
Frequently Asked Questions — Stainless Steel ER309L Filler Wire
Technical questions and answers regarding classification, base metal compatibility, welding parameters and procurement for Stainless Steel ER309L Filler Wire:
Stainless Steel ER309L Filler Wire is classified under AWS A5.9 / ASME SFA-5.9 ER309L and EN ISO 14343-A W/G 23 12 L (W.Nr. 1.4332) (UNS UNS S30983, Werkstoff Nr. 1.4332). Contact us for confirmed product specifications and available technical documentation.
Stainless Steel ER309L Filler Wire (AWS A5.9 / ASME SFA-5.9 ER309L) is engineered for welding Dissimilar joints between AISI 304 / 304L / 316 / 316L / 321 / 347 stainless steels and carbon/low-alloy steels (ASTM A516 Gr.70, A106 Gr.B, A36, A387); joining clad steel plates; and welding wrought/cast 309S / 309Cb base metals.
Stainless Steel ER309L Filler Wire is supplied for GTAW (TIG), GMAW (MIG), SAW as precision layer-wound MIG spools (0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm) and straight cut-length TIG rods (1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm in 914mm / 36-inch and 1000mm lengths). Recommended shielding gas: 100% Argon (GTAW); Ar + 1–2% O2 or Ar + 2% CO2 (GMAW).
When welding carbon steel to stainless steel with ER309L, control arc placement and heat input to keep carbon steel dilution below 30%. Note: If the dissimilar joint will operate continuously above 315–425°C or undergo high-temperature Post-Weld Heat Treatment (PWHT), specify Inconel 82 (ERNiCr-3) or Inconel 625 (ERNiCrMo-3) instead of ER309L to avoid carbon migration and thermal expansion fatigue. Typical applications include: Welding carbon steel pipe supports, structural clips, skirts and saddles onto 304L/316L stainless steel pressure vessels; First-layer barrier weld overlay cladding on carbon steel reactor shells and heat exchanger tubesheets (prior to ER308L or ER316L cap layers); Joining the stainless-clad side of roll-bonded or explosion-bonded clad pressure vessel plates.
International B2B Technical Enquiry & Quotation Request
Submit your alloy grade, AWS/ISO classification, diameter, welding process and delivery destination. Our technical export team in Mumbai responds to enquiries from the Middle East, GCC, USA, UK, Europe, Singapore, Sri Lanka, South Africa, Peru and global markets.