Stainless Steel ER308L Filler Wire Supplier — AWS A5.9 ER308L TIG & MIG Wire
Low-carbon (0.03% max C) 19Cr-9Ni austenitic stainless steel filler wire (AWS A5.9 ER308L / UNS S30883) engineered for intergranular-corrosion-resistant welding of AISI 304, 304L, 321 and 347 stainless steels.
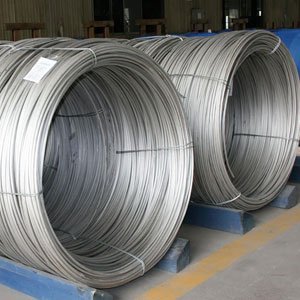
Extra-Low Carbon 19Cr-9Ni Filler Wire for Sensitization-Free 304/304L Welding
Stainless Steel ER308L Filler Wire (classified under AWS A5.9 ER308L and EN ISO 14343-A 19 9 L) is the primary austenitic stainless steel welding consumable for joining AISI 304 and 304L (18Cr-8Ni) base metals. By restricting carbon content to 0.03% maximum, ER308L prevents intergranular chromium carbide precipitation (sensitization) in the weld metal without requiring niobium or titanium stabilizers, allowing welded assemblies to enter corrosive service in the as-welded condition.
Our ER308L chemistry is balanced to solidify in the primary ferritic-austenitic mode with a controlled delta-ferrite content (typically 4–10 FN), providing high resistance to hot solidification cracking while preserving excellent Charpy impact toughness down to cryogenic temperatures (-196°C).
Alloy Identification, Standards & Supply Specifications
Controlled Cr/Ni ratio ensures optimal delta-ferrite for crack immunity without risking brittle sigma-phase formation during service.
| Product Designation | Stainless Steel ER308L Filler Wire (TIG Welding Rod / MIG Spooled Wire) |
|---|---|
| AWS / ASME Classification | AWS A5.9 / ASME SFA-5.9 ER308L |
| EN / ISO Classification | EN ISO 14343-A W/G 19 9 L (W.Nr. 1.4316) |
| UNS Designation & Werkstoff Nr. | UNS S30883 • W.Nr. 1.4316 |
| Compatible Base Materials | AISI 304, 304L, 304LN (UNS S30400, S30403), ASTM A240 / A312 TP304/TP304L, CF3 / CF8 cast stainless steels, and AISI 321 / 347 for service temperatures below 350°C. |
| Supported Welding Processes | GTAW (TIG), GMAW (MIG), SAW |
| Shielding Gas Recommendations | 100% Argon (GTAW); Ar + 1–2% O2 or Ar + 2% CO2 (GMAW) |
| Available Wire Diameters | MIG Spools: 0.8mm (.030"), 0.9mm (.035"), 1.0mm (.040"), 1.2mm (.045"), 1.6mm (1/16") TIG Cut-Length Rods: 1.2mm, 1.6mm (1/16"), 2.0mm, 2.4mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32") × 914mm (36") / 1000mm |
| Packaging & Storage | TIG Rods: 5 kg / 10 kg moisture-resistant tubular plastic packs in export master cartons. MIG Wire: 12.5 kg / 15 kg precision layer-wound BS300 / S200 spools sealed in VCI polyethylene film. Storage: Store in a dry, temperature-controlled indoor store (+10°C to +40°C, <60% RH) in original sealed packaging. |
Chemical Composition Specification (AWS A5.9 / ASME SFA-5.9 ER308L)
The table below specifies the standard wire chemical composition limits in weight percent (wt.%). Single values represent maximum permissible limits unless stated otherwise:
| Element | Verified Specification Limit (wt.%) | Metallurgical Function in Weld Metal |
|---|---|---|
| Carbon (C) | 0.03 max | Extra-low carbon prevents intergranular carbide precipitation |
| Chromium (Cr) | 19.5 – 22.0 | Forms passive Cr2O3 surface film for atmospheric and nitric acid resistance |
| Nickel (Ni) | 9.0 – 11.0 | Stabilizes the austenitic matrix and provides cryogenic toughness |
| Manganese (Mn) | 1.0 – 2.5 | Assists deoxidation and resists hot solidification cracking |
| Silicon (Si) | 0.30 – 0.65 (ER308LSi: 0.65–1.00) | Controls weld pool fluidity and bead wetting |
| Molybdenum (Mo) | 0.75 max | Residual limit per AWS A5.9 |
| Copper (Cu) | 0.75 max | Residual limit per AWS A5.9 |
| Phosphorus (P) & Sulfur (S) | P ≤ 0.030, S ≤ 0.030 | Strictly limited to prevent solidification microfissuring |
| Iron (Fe) | Remainder | Austenitic-ferritic matrix balance |
Mechanical & Physical Properties
The values below distinguish between minimum AWS/ISO classification requirements for all-weld-metal test assemblies and typical as-welded deposited weld metal benchmarks:
| Property | Value | Unit | Specification / Reference Basis |
|---|---|---|---|
| Tensile Strength | ≥ 520 (Typical: 570 – 610) | MPa | Typical All-Weld-Metal Deposit (AWS A5.9 / ISO 14343) |
| Yield Strength (0.2% Offset) | ≥ 350 (Typical: 400 – 440) | MPa | Typical As-Welded GTAW/GMAW Deposit |
| Elongation | ≥ 35 (Typical: 40 – 45) | % | In 5D / 50 mm Gauge Length |
| Charpy V-Notch Impact (-196°C) | ≥ 47 (Typical: 65 – 95) | J | Typical GTAW Weld Metal Toughness |
| Ferrite Number (FN) | 4 – 10 | FN | Typical WRC-1992 Constitution Diagram Range |
| Density | 7.90 | g/cm³ | Physical Property Reference |
Corrosion Resistance, Welding Considerations & Industrial Applications
ER308L filler wire resists nitric acid, organic acids, food/beverage media and atmospheric exposure. Do not preheat; keep interpass temperatures below 150°C (300°F), use stainless steel wire brushes exclusively, and apply pure Argon back-purging on sanitary and process pipe root runs.
Typical Industrial Applications
- Chemical, petrochemical and nitric acid storage tanks, piping and heat exchangers (304/304L)
- Cryogenic LNG piping, liquid nitrogen/oxygen storage vessels and cold-box equipment
- Food, dairy, brewery, wine and commercial kitchen sanitary stainless steel equipment
- Pharmaceutical clean-steam and water-for-injection (WFI) skids and architectural stainless structures
International Enquiry Destinations
FillerWires welcomes B2B export enquiries for Stainless Steel ER308L Filler Wire from EPC contractors, process equipment fabricators, shipyards and distributors across the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Typical Regional Sector Demand |
|---|---|---|
| United Arab Emirates | Dubai, Abu Dhabi, Sharjah, Ajman, Jebel Ali | Process skids, architectural stainless & food machinery |
| Oman, Saudi Arabia & Qatar | Muscat, Sohar, Riyadh, Dammam, Jeddah, Doha, Ras Laffan | LNG cryogenic lines, water tanks & industrial piping |
| Kuwait & Bahrain | Kuwait City, Shuwaikh, Ahmadi, Manama, Hidd | Refinery utility piping & commercial fabrication |
| United States & United Kingdom | Houston, Chicago, Los Angeles, Birmingham, Manchester, Glasgow | Food/dairy tanks, cryogenic vessels & general shop fabrication |
| Italy, Germany & Europe | Milan, Bologna, Parma, Turin, Hamburg, Munich, Rotterdam, Warsaw | Hygienic food/packaging machinery & pressure vessels |
| Sri Lanka, Singapore, South Africa & Peru | Colombo, Galle, Jurong, Tuas, Johannesburg, Cape Town, Lima | Tea/dairy/beverage plants, marine & industrial fabrication |
Frequently Asked Questions — Stainless Steel ER308L Filler Wire
Technical questions and answers regarding classification, base metal compatibility, welding parameters and procurement for Stainless Steel ER308L Filler Wire:
Stainless Steel ER308L Filler Wire is classified under AWS A5.9 / ASME SFA-5.9 ER308L and EN ISO 14343-A W/G 19 9 L (W.Nr. 1.4316) (UNS UNS S30883, Werkstoff Nr. 1.4316). Contact us for confirmed product specifications and available technical documentation.
Stainless Steel ER308L Filler Wire (AWS A5.9 / ASME SFA-5.9 ER308L) is engineered for welding AISI 304, 304L, 304LN (UNS S30400, S30403), ASTM A240 / A312 TP304/TP304L, CF3 / CF8 cast stainless steels, and AISI 321 / 347 for service temperatures below 350°C.
Stainless Steel ER308L Filler Wire is supplied for GTAW (TIG), GMAW (MIG), SAW as precision layer-wound MIG spools (0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm) and straight cut-length TIG rods (1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm in 914mm / 36-inch and 1000mm lengths). Recommended shielding gas: 100% Argon (GTAW); Ar + 1–2% O2 or Ar + 2% CO2 (GMAW).
ER308L filler wire resists nitric acid, organic acids, food/beverage media and atmospheric exposure. Do not preheat; keep interpass temperatures below 150°C (300°F), use stainless steel wire brushes exclusively, and apply pure Argon back-purging on sanitary and process pipe root runs. Typical applications include: Chemical, petrochemical and nitric acid storage tanks, piping and heat exchangers (304/304L); Cryogenic LNG piping, liquid nitrogen/oxygen storage vessels and cold-box equipment; Food, dairy, brewery, wine and commercial kitchen sanitary stainless steel equipment.
International B2B Technical Enquiry & Quotation Request
Submit your alloy grade, AWS/ISO classification, diameter, welding process and delivery destination. Our technical export team in Mumbai responds to enquiries from the Middle East, GCC, USA, UK, Europe, Singapore, Sri Lanka, South Africa, Peru and global markets.