AWS A5.14 ERNiCrMo-3
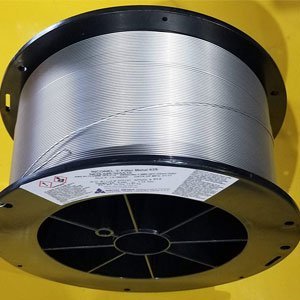
Inconel 625 Filler Wire
Ni-22Cr-9Mo-3.5Nb filler wire for sour gas weld overlay cladding, 6% Mo super-austenitic stainless steel welding and cryogenic-to-980°C service.
AWS A5.14 / ASME SFA-5.14 nickel-base bare welding filler wires and TIG rods engineered for sour oil & gas cladding, severe chemical corrosion, cryogenic service and high-temperature oxidation resistance.
FillerWires supplies nickel and nickel-alloy welding filler metals classified under AWS A5.14 / ASME SFA-5.14 and EN ISO 18274. Nickel alloys tolerate higher alloy additions of chromium, molybdenum, tungsten, copper and cobalt in solid solution than iron-base stainless steels, making them indispensable for weld overlay cladding on subsea oil & gas equipment, dissimilar metal joining, flue-gas desulfurization (FGD) scrubbers, sulfuric/hydrochloric acid reactors and 1100°C petrochemical furnaces.
Contact us for confirmed product specifications and available technical documentation.
Ni-22Cr-9Mo-3.5Nb filler wire for sour gas weld overlay cladding, 6% Mo super-austenitic stainless steel welding and cryogenic-to-980°C service.
Ni-Fe-Cr-Mo-Cu filler metal resistant to sulfuric acid, phosphoric acid, sour gas and chloride stress-corrosion cracking.
Ni-20Cr-3Mn-2.5Nb wire for welding Alloy 600, Incoloy 800/800HT and dissimilar joints between nickel alloys, stainless and carbon steels.
Ni-22Cr-12.5Co-9Mo-1.2Al filler wire for extreme creep strength and oxidation/carburization resistance up to 1100°C.

Ni-16Mo-15.5Cr-4W low-carbon filler wire resisting wet chlorine gas, ferric/cupric chlorides, hot contaminated acids and FGD scrubbers.

Ni-22Cr-13Mo-3W filler wire providing balanced resistance to both oxidizing and reducing acid streams and localized pitting/crevice attack.
Nickel-copper filler metals for Monel 400 marine splash-zone sheathing, hydrofluoric acid alkylation units and brine evaporators.
Niobium-stabilized Ni-Cr-Mo-Cu filler metal engineered for sulfuric acid tanks, heat exchangers and chemical process piping.
High thermal-stability Ni-16Cr-16Mo-Ti filler wire (ERNiCrMo-7 / UNS N06455) resisting intermetallic phase precipitation in the weld HAZ.
Nickel-chromium-iron niobium-bearing welding wire (AMS 5679 / ERNiCrFe-5) for joining Inconel 600 and high-temperature aerospace/furnace alloys.
Commercially pure nickel filler wire with titanium deoxidizer for welding Nickel 200 and 201 in caustic soda evaporators and chlor-alkali plants.
Comparison of AWS A5.14 / EN ISO 18274 classifications, UNS designations and nominal chemical compositions across our nickel alloy range. Contact us for confirmed product specifications and available technical documentation.
| Product Designation | AWS Classification | UNS No. | Nominal Composition (wt.%) | Min. Tensile Strength (AWS) | Primary Industrial Application |
|---|---|---|---|---|---|
| Inconel 625 | AWS A5.14 ERNiCrMo-3 | N06625 | 61Ni – 21.5Cr – 9Mo – 3.6(Nb+Ta) | 760 MPa (110 ksi) | Offshore cladding, sour gas, 6Mo super-austenitic & dissimilar welds |
| Inconel 825 | AWS A5.14 ERNiFeCr-1 (or ERNiCrMo-3 overmatch) | N08825 | 42Ni – 30Fe – 21.5Cr – 3Mo – 2.2Cu – 0.9Ti | 550 MPa (80 ksi) | Sulfuric & phosphoric acid piping, pickling equipment, sour service |
| Inconel 82 | AWS A5.14 ERNiCr-3 | N06082 | 72Ni – 20Cr – 3Mn – 2.5(Nb+Ta) | 550 MPa (80 ksi) | Alloy 600/800HT welding & dissimilar stainless-to-carbon/nickel joints |
| Inconel 617 | AWS A5.14 ERNiCrCoMo-1 | N06617 | 52Ni – 22Cr – 12.5Co – 9Mo – 1.2Al | 620 MPa (90 ksi) | Gas turbines, ethylene pyrolysis & reforming furnaces up to 1100°C |
| Hastelloy C276 | AWS A5.14 ERNiCrMo-4 | N10276 | 57Ni – 16Mo – 15.5Cr – 5.5Fe – 3.8W | 690 MPa (100 ksi) | Chemical reactors, wet chlorine, FGD scrubbers & sour downhole tools |
| Hastelloy C22 | AWS A5.14 ERNiCrMo-10 | N06022 | 56Ni – 22Cr – 13Mo – 3W – 3Fe | 690 MPa (100 ksi) | Mixed oxidizing/reducing acid streams, pharmaceutical & waste incineration |
| Hastelloy C4 | AWS A5.14 ERNiCrMo-7 | N06455 | 65Ni – 16Cr – 16Mo – ≤0.7Ti | 690 MPa (100 ksi) | Hot mineral acids & high-thermal-stability chemical process welds |
| Monel 400 (Filler Metal 60) | AWS A5.14 ERNiCu-7 | N04060 | 65Ni – 30Cu – 3.5Mn – 2.2Ti | 480 MPa (70 ksi) | Seawater splash zones, HF alkylation units & Monel 400 vessels |
| Pure Nickel 200 (Filler Metal 61) | AWS A5.14 ERNi-1 | N02061 | 96Ni – 2.8Ti – ≤1.0Mn | 410 MPa (60 ksi) | Caustic soda evaporators, chlor-alkali & Nickel 200/201 joining |
FillerWires welcomes technical and procurement enquiries for Inconel, Hastelloy, Monel and pure nickel welding wires from the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Primary Nickel Alloy Applications |
|---|---|---|
| United Arab Emirates (UAE) | Dubai, Abu Dhabi, Sharjah, Jebel Ali, Fujairah | Subsea & offshore sour-service weld overlay cladding (ERNiCrMo-3 / Inconel 625, Inconel 825) |
| Oman | Muscat, Sohar, Salalah, Duqm | Refinery, LNG & petrochemical heat exchangers (Inconel 625, Hastelloy C276, Monel 400) |
| Saudi Arabia | Dammam, Jubail, Riyadh, Yanbu, Jeddah, Khobar, Dhahran | Downstream crackers, sour gas & acid plants (Inconel 625, Inconel 617, Inconel 82, C276) |
| Qatar, Kuwait & Bahrain | Doha, Ras Laffan, Mesaieed, Kuwait City, Ahmadi, Shuaiba, Manama, Hidd | Cryogenic LNG piping, offshore splash zones & reformer tubes (Inconel 625, Monel 400, Inconel 617) |
| United States & United Kingdom | Houston, Pittsburgh, Chicago, Los Angeles, Aberdeen, Sheffield, Birmingham | Gulf Coast & North Sea oilfield equipment, chemical processing & turbine manufacturing |
| Germany, Italy & Netherlands | Hamburg, Düsseldorf, Essen, Milan, Turin, Genoa, Rotterdam, Eindhoven | PED/ASME chemical reactors, waste-to-energy boiler cladding & offshore fabrication |
| Singapore, South Africa & Peru | Jurong, Tuas, Johannesburg, Durban, Richards Bay, Lima, Callao, Arequipa | FPSO topsides, synfuels, sulfuric/phosphoric acid leaching & mining autoclaves |
Engineering questions on AWS A5.14 Inconel, Hastelloy, Monel and pure nickel welding consumables.
Bare nickel and nickel-alloy welding rods and spooled electrodes are classified under AWS A5.14 / ASME SFA-5.14 and EN ISO 18274. Key grades include ERNiCrMo-3 (Inconel 625), ERNiCr-3 (Inconel 82), ERNiCrCoMo-1 (Inconel 617), ERNiFeCr-1 (Inconel 825), ERNiCrMo-4 (Hastelloy C276), ERNiCrMo-10 (Hastelloy C22) and ERNiCu-7 (Monel 400).
Inconel 625 (ERNiCrMo-3) contains ~9% Molybdenum and ~3.6% Niobium in a high-nickel matrix, providing a Pitting Resistance Equivalent Number (PREN) above 50. This prevents localized pitting in sour oilfield cladding and compensates for molybdenum segregation when welding 6% Mo super-austenitic stainless steels.
Nickel alloys do not require preheating above ambient room temperature. For corrosion-resistant Ni-Cr-Mo alloys such as Hastelloy C276 and C22, interpass temperatures should be maintained below 95°C–120°C using stringer beads to prevent secondary phase precipitation in the weld heat-affected zone.