Inconel 617 Filler Wire Supplier — AWS A5.14 ERNiCrCoMo-1 Welding Wire
Solid-solution Nickel-Chromium-Cobalt-Molybdenum-Aluminum filler wire (AWS A5.14 ERNiCrCoMo-1 / UNS N06617) for extreme creep-rupture strength and oxidation/carburization resistance up to 1100°C.
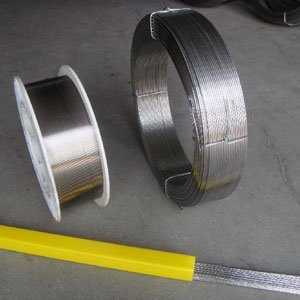
Ultra-High-Temperature Creep & Carburization Resistant Ni-Cr-Co-Mo-Al Filler Metal
Inconel 617 Filler Wire (AWS A5.14 ERNiCrCoMo-1 / Alloy 617 Filler Metal) is a premier solid-solution strengthened nickel-chromium-cobalt-molybdenum alloy engineered for structural weld integrity at temperatures from 800°C to 1100°C (1470°F to 2010°F). Cobalt (10.0–15.0%) and molybdenum (8.0–10.0%) provide extraordinary high-temperature creep-rupture strength, while high chromium (20.0–24.0%) combined with aluminum (0.80–1.50%) forms a protective subsurface alumina/chromia scale.
Inconel 617 filler metal is widely specified for welding Alloy 617, Incoloy 800H/800HT, Alloy 602CA and cast HP/HK heat-resistant alloys in ethylene cracking furnaces, steam methane reformer manifolds, gas turbine combustion cans, nitric acid catalyst grids and ultra-supercritical (A-USC) power plant headers.
Alloy Identification, Standards & Supply Specifications
Because Inconel 617 contains 0.8–1.5% Aluminum, meticulous inter-pass wire brushing (using dedicated stainless steel brushes) and inert gas shielding are required to remove thin refractory aluminum oxide films between passes.
| Product Designation | Inconel 617 Filler Wire (TIG Welding Rod / MIG Spooled Wire) |
|---|---|
| AWS / ASME Classification | AWS A5.14 ERNiCrCoMo-1 |
| EN / ISO Classification | EN ISO 18274 S Ni 6617 (NiCr22Co12Mo9) |
| UNS Designation & Werkstoff Nr. | UNS N06617 • W.Nr. 2.4627 (Base Metal: 2.4663) |
| Compatible Base Materials | Inconel 617 (UNS N06617), Incoloy 800H / 800HT (N08810 / N08811), Inconel 600 / 601, Haynes 230 (dissimilar), and cast heat-resistant alloys (HP-Mod, HK-40) in furnace and turbine service. |
| Supported Welding Processes | GTAW (TIG), GMAW (Pulsed / Spray MIG) |
| Shielding Gas Recommendations | 100% Argon or Ar + He (GTAW); Ar + He (Pulsed GMAW) |
| Available Wire Diameters | MIG Spools: 0.8mm (.030"), 0.9mm (.035"), 1.0mm (.040"), 1.2mm (.045"), 1.6mm (1/16") TIG Cut-Length Rods: 1.2mm, 1.6mm (1/16"), 2.0mm, 2.4mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32") × 914mm (36") / 1000mm |
| Packaging & Storage | TIG Rods: 5 kg / 10 kg moisture-resistant tubular plastic packs in export master cartons. MIG Wire: 12.5 kg / 15 kg precision layer-wound BS300 / S200 spools sealed in VCI polyethylene film. Storage: Store in a dry, temperature-controlled indoor store (+10°C to +40°C, <60% RH) in original sealed packaging. |
Chemical Composition Specification (AWS A5.14 ERNiCrCoMo-1)
The table below specifies the standard wire chemical composition limits in weight percent (wt.%). Single values represent maximum permissible limits unless stated otherwise:
| Element | Verified Specification Limit (wt.%) | Metallurgical Function in Weld Metal |
|---|---|---|
| Nickel (Ni) | 44.5 min (Balance ~52%) | Stable high-temperature austenitic base matrix |
| Chromium (Cr) | 20.0 – 24.0 | Primary oxidation, sulfidation and hot-gas corrosion barrier |
| Cobalt (Co) | 10.0 – 15.0 | Solid-solution strengthening and creep-rupture stability >850°C |
| Molybdenum (Mo) | 8.0 – 10.0 | Matrix strengthening and creep resistance at extreme temperatures |
| Aluminum (Al) | 0.80 – 1.50 | Forms protective Al2O3 subscale against oxidation and carburization |
| Carbon (C) | 0.05 – 0.15 | Controlled carbon forms stable carbides for high-temperature creep strength |
| Iron (Fe) | 3.0 max | Controlled low iron |
| Manganese (Mn) & Silicon (Si) | Mn ≤ 1.0, Si ≤ 1.0 | Deoxidation and fluidity control |
| Titanium (Ti) & Copper (Cu) | Ti ≤ 0.60, Cu ≤ 0.50 | Minor stabilizing and residual limits |
| Sulfur (S) | 0.015 max | Strictly controlled to prevent grain-boundary embrittlement |
Mechanical & Physical Properties
The values below distinguish between minimum AWS/ISO classification requirements for all-weld-metal test assemblies and typical as-welded deposited weld metal benchmarks:
| Property | Value | Unit | Specification / Reference Basis |
|---|---|---|---|
| Tensile Strength | ≥ 620 (Typical: 750 – 810) | MPa | AWS A5.14 Minimum / Typical All-Weld-Metal |
| Yield Strength (0.2% Offset) | ≥ 400 (Typical: 470 – 520) | MPa | Typical As-Welded GTAW Deposit |
| Elongation | ≥ 25 (Typical: 32 – 38) | % | AWS A5.14 Minimum in 4D |
| Density | 8.36 | g/cm³ | Physical Property Reference |
| Melting Range | 1330 – 1380 | °C | Physical Property Reference |
Corrosion Resistance, Welding Considerations & Industrial Applications
Inconel 617 filler wire resists cyclic oxidation, carburization, metal dusting and nitriding at temperatures up to 1100°C. Use low-to-moderate heat input, stringer beads, extended gas post-flow to protect the hot tungsten electrode and weld crater from oxidation, and brush any surface oxide film clean between passes.
Typical Industrial Applications
- Gas turbine combustion cans, transition ducts and exhaust liners in power and aviation turbines
- Ethylene pyrolysis furnace coils, transfer line exchangers (TLE) and steam methane reformer headers/pigtails
- Nitric acid plant catalyst support grids and high-temperature heat exchangers
- Industrial heat-treating furnaces, radiant tubes, muffles and strand annealing lines
- Joining Incoloy 800HT where higher weld metal creep strength than ERNiCr-3 (Inconel 82) is required (>800°C)
International Enquiry Destinations
FillerWires welcomes B2B export enquiries for Inconel 617 Filler Wire from EPC contractors, process equipment fabricators, shipyards and distributors across the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Typical Regional Sector Demand |
|---|---|---|
| Saudi Arabia | Jubail, Yanbu, Dammam, Riyadh | Ethylene crackers, methanol/ammonia reformers & gas turbines |
| Qatar & Bahrain | Ras Laffan, Mesaieed, Doha, Manama, Sitra | Gas-to-Liquids (GTL), LNG power turbines &アルミ/refining furnaces |
| United Arab Emirates & Oman | Abu Dhabi, Ruwais, Dubai, Sohar, Duqm | Petrochemical pyrolysis furnaces & power generation |
| United States & United Kingdom | Houston, Greenville/Atlanta, Cincinnati, Derby, Aberdeen, Sheffield | Gas turbine manufacturing, aerospace & petrochemical furnaces |
| Germany, Italy & Netherlands | Mülheim/Essen, Düsseldorf, Milan, Turin, Genoa, Rotterdam | Turbine engineering, reformer manifolds & furnace fabrication |
| Singapore, South Africa & Peru | Jurong Island, Secunda/Johannesburg, Lima, Talara | Refinery heaters, synfuel reformers & power plants |
Frequently Asked Questions — Inconel 617 Filler Wire
Technical questions and answers regarding classification, base metal compatibility, welding parameters and procurement for Inconel 617 Filler Wire:
Inconel 617 Filler Wire is classified under AWS A5.14 ERNiCrCoMo-1 and EN ISO 18274 S Ni 6617 (NiCr22Co12Mo9) (UNS UNS N06617, Werkstoff Nr. 2.4627 (Base Metal: 2.4663)). Contact us for confirmed product specifications and available technical documentation.
Inconel 617 Filler Wire (AWS A5.14 ERNiCrCoMo-1) is engineered for welding Inconel 617 (UNS N06617), Incoloy 800H / 800HT (N08810 / N08811), Inconel 600 / 601, Haynes 230 (dissimilar), and cast heat-resistant alloys (HP-Mod, HK-40) in furnace and turbine service.
Inconel 617 Filler Wire is supplied for GTAW (TIG), GMAW (Pulsed / Spray MIG) as precision layer-wound MIG spools (0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm) and straight cut-length TIG rods (1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm in 914mm / 36-inch and 1000mm lengths). Recommended shielding gas: 100% Argon or Ar + He (GTAW); Ar + He (Pulsed GMAW).
Inconel 617 filler wire resists cyclic oxidation, carburization, metal dusting and nitriding at temperatures up to 1100°C. Use low-to-moderate heat input, stringer beads, extended gas post-flow to protect the hot tungsten electrode and weld crater from oxidation, and brush any surface oxide film clean between passes. Typical applications include: Gas turbine combustion cans, transition ducts and exhaust liners in power and aviation turbines; Ethylene pyrolysis furnace coils, transfer line exchangers (TLE) and steam methane reformer headers/pigtails; Nitric acid plant catalyst support grids and high-temperature heat exchangers.
International B2B Technical Enquiry & Quotation Request
Submit your alloy grade, AWS/ISO classification, diameter, welding process and delivery destination. Our technical export team in Mumbai responds to enquiries from the Middle East, GCC, USA, UK, Europe, Singapore, Sri Lanka, South Africa, Peru and global markets.