Monel Filler Wires Supplier — Monel 400 (ERNiCu-7) & Monel 67 Welding Wire
Nickel-Copper (ERNiCu-7 / Filler Metal 60) and Copper-Nickel (Monel 67) welding filler wires engineered for marine splash-zone sheathing, hydrofluoric acid alkylation units, desalination plants and brine evaporators.
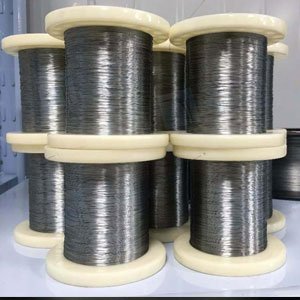
Nickel-Copper Welding Consumables for Flowing Seawater, Splash Zones & Hydrofluoric Acid
Monel Filler Wires encompass two essential nickel-copper welding consumables: Monel Filler Metal 60 (AWS A5.14 ERNiCu-7 / UNS N04060) for welding Monel 400 (UNS N04400) and Monel R-405, and Monel Filler Metal 67 (70Cu-30Ni / ERCuNi type) for joining copper-nickel alloys and dissimilar Monel-to-CuNi marine systems. Monel 400 filler wire contains ~65% Nickel, ~30% Copper, 3.5% Manganese and 1.5–3.0% Titanium, where titanium acts as a critical deoxidizer and nitrogen scavenger to eliminate porosity during arc welding.
Monel 400 weld deposits exhibit extraordinary resistance to high-velocity flowing seawater, marine splash-zone corrosion on offshore platform risers and legs, brackish water, chlorinated solvents, alkalies and hydrofluoric (HF) acid in refinery alkylation units.
Alloy Identification, Standards & Supply Specifications
When overlaying or welding Monel 400 directly onto carbon steel where iron dilution exceeds 10–15%, apply a pure nickel (ERNi-1 / Filler Metal 61) or ERNiCr-3 buffer layer first to prevent copper-induced hot cracking.
| Product Designation | Monel 400 & Monel 67 Filler Wires (TIG Welding Rod / MIG Spooled Wire) |
|---|---|
| AWS / ASME Classification | AWS A5.14 ERNiCu-7 (Monel 60) / AWS A5.7 ERCuNi (Monel 67) |
| EN / ISO Classification | EN ISO 18274 S Ni 4060 (NiCu30Mn3Ti) |
| UNS Designation & Werkstoff Nr. | UNS N04060 (ERNiCu-7) / UNS C71580 (Filler 67) • W.Nr. 2.4377 (Base: 2.4360) |
| Compatible Base Materials | Monel Alloy 400 (UNS N04400 / W.Nr. 2.4360), Monel R-405 (N04405), Copper-Nickel alloys (70/30 and 90/10 with Monel 67), and clad Monel 400 vessels (with appropriate nickel buffer). |
| Supported Welding Processes | GTAW (TIG), GMAW (MIG), SAW |
| Shielding Gas Recommendations | 100% Argon (GTAW); Argon or Argon + Helium (GMAW) |
| Available Wire Diameters | MIG Spools: 0.8mm (.030"), 0.9mm (.035"), 1.0mm (.040"), 1.2mm (.045"), 1.6mm (1/16") TIG Cut-Length Rods: 1.2mm, 1.6mm (1/16"), 2.0mm, 2.4mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32") × 914mm (36") / 1000mm |
| Packaging & Storage | TIG Rods: 5 kg / 10 kg moisture-resistant tubular plastic packs in export master cartons. MIG Wire: 12.5 kg / 15 kg precision layer-wound BS300 / S200 spools sealed in VCI polyethylene film. Storage: Store in a dry, temperature-controlled indoor store (+10°C to +40°C, <60% RH) in original sealed packaging. |
Chemical Composition Specification (AWS A5.14 ERNiCu-7 (Monel 60) / AWS A5.7 ERCuNi (Monel 67))
The table below specifies the standard wire chemical composition limits in weight percent (wt.%). Single values represent maximum permissible limits unless stated otherwise:
| Element | Verified Specification Limit (wt.%) | Metallurgical Function in Weld Metal |
|---|---|---|
| Nickel + Cobalt (Ni+Co) | 62.0 – 69.0 (ERNiCu-7) | Primary matrix providing alkali, HF acid and chloride SCC resistance |
| Copper (Cu) | Remainder (~28 – 32%) | Solid-solution partner enhancing seawater and reducing-acid resistance |
| Manganese (Mn) | 4.0 max (Typical: 3.0 – 4.0) | Prevents hot microfissuring and assists weld pool deoxidation |
| Titanium (Ti) | 1.5 – 3.0 | Essential deoxidizer/denitrider preventing weld metal gas porosity |
| Iron (Fe) | 2.5 max | Controlled iron enhances cavitation-erosion resistance |
| Silicon (Si) | 1.25 max | Fluidity and deoxidation control |
| Carbon (C) | 0.15 max | Standard limit per AWS A5.14 |
| Aluminum (Al) | 1.25 max | Auxiliary deoxidizer |
| Phosphorus (P) & Sulfur (S) | P ≤ 0.020, S ≤ 0.015 | Strict impurity limits |
Mechanical & Physical Properties
The values below distinguish between minimum AWS/ISO classification requirements for all-weld-metal test assemblies and typical as-welded deposited weld metal benchmarks:
| Property | Value | Unit | Specification / Reference Basis |
|---|---|---|---|
| Tensile Strength | ≥ 480 (Typical: 510 – 550) | MPa | AWS A5.14 ERNiCu-7 Minimum / Typical |
| Yield Strength (0.2% Offset) | ≥ 200 (Typical: 230 – 270) | MPa | Typical As-Welded GTAW Deposit |
| Elongation | ≥ 30 (Typical: 35 – 40) | % | AWS A5.14 Minimum in 4D |
| Density | 8.80 | g/cm³ | Physical Property Reference |
| Melting Range | 1300 – 1350 | °C | Physical Property Reference |
Product Comparison: Monel 400 (ERNiCu-7 / FM 60) vs. Monel 67 Filler Wire
| Attribute | Monel 400 / Filler Metal 60 (AWS A5.14 ERNiCu-7) | Monel 67 Filler Wire (AWS A5.7 ERCuNi Type) |
|---|---|---|
| Nominal Alloy Balance | ~65% Nickel – 30% Copper – 3.5% Mn – 2.2% Ti | ~67% Copper – 30% Nickel – 0.6% Fe – 0.8% Mn – 0.35% Ti |
| Primary Base Metals | Monel 400 (UNS N04400) & Monel R-405 | 70/30 & 90/10 Cupro-Nickel and CuNi-to-Monel 400 joints |
| Minimum Tensile Strength | 480 MPa (70 ksi) | 345 MPa (50 ksi) |
| Core Industrial Duty | Offshore riser splash-zone sheathing, HF acid alkylation, salt evaporators | Seawater desalination piping, marine condensers, ship hulls |
Corrosion Resistance, Welding Considerations & Industrial Applications
Monel 400 filler wire offers unmatched durability in the splash and tidal zones of offshore oil & gas platforms, where alternating wet and dry aerated seawater rapidly corrodes steel. In refinery hydrofluoric (HF) acid alkylation units, ERNiCu-7 is the standard consumable for welding Monel 400 fractionator columns, valves and piping.
Typical Industrial Applications
- Offshore oil & gas platform riser and jacket splash-zone Monel 400 sheathing in the Arabian Gulf and North Sea
- Refinery hydrofluoric (HF) acid alkylation columns, reboilers, valves and piping
- Multi-Stage Flash (MSF) desalination brine heaters, demisters and vacuum salt evaporators
- Marine propeller shafts, seawater pump impellers and naval hull fittings
- Uranium refining and fluorination chemical processing equipment
International Enquiry Destinations
FillerWires welcomes B2B export enquiries for Monel 400 & Monel 67 Filler Wires from EPC contractors, process equipment fabricators, shipyards and distributors across the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Typical Regional Sector Demand |
|---|---|---|
| Qatar & United Arab Emirates | Doha, Ras Laffan, Abu Dhabi, Dubai, Sharjah, Fujairah | Offshore platform splash-zone sheathing & LNG marine systems |
| Saudi Arabia & Kuwait | Dammam, Jubail, Ras Tanura, Yanbu, Ahmadi, Shuaiba | Refinery HF alkylation units & offshore jackets |
| Oman & Bahrain | Muscat, Sohar, Duqm, Salalah, Manama, Hidd, Sitra | Desalination brine heaters & shiprepair drydocks |
| United States & United Kingdom | Houston, Corpus Christi, New Orleans, Aberdeen, Southampton | Gulf Coast HF alkylation refineries & offshore rigs |
| Italy, Netherlands & Norway | Genoa, Milan, Venice, Rotterdam, Stavanger, Bergen | Marine heat exchangers, refineries & offshore platforms |
| Singapore, Sri Lanka & Peru | Jurong, Tuas, Colombo, Callao, Talara | FPSO marine conversion & refinery maintenance |
Frequently Asked Questions — Monel 400 & Monel 67 Filler Wires
Technical questions and answers regarding classification, base metal compatibility, welding parameters and procurement for Monel 400 & Monel 67 Filler Wires:
Monel 400 & Monel 67 Filler Wires is classified under AWS A5.14 ERNiCu-7 (Monel 60) / AWS A5.7 ERCuNi (Monel 67) and EN ISO 18274 S Ni 4060 (NiCu30Mn3Ti) (UNS UNS N04060 (ERNiCu-7) / UNS C71580 (Filler 67), Werkstoff Nr. 2.4377 (Base: 2.4360)). Contact us for confirmed product specifications and available technical documentation.
Monel 400 & Monel 67 Filler Wires (AWS A5.14 ERNiCu-7 (Monel 60) / AWS A5.7 ERCuNi (Monel 67)) is engineered for welding Monel Alloy 400 (UNS N04400 / W.Nr. 2.4360), Monel R-405 (N04405), Copper-Nickel alloys (70/30 and 90/10 with Monel 67), and clad Monel 400 vessels (with appropriate nickel buffer).
Monel 400 & Monel 67 Filler Wires is supplied for GTAW (TIG), GMAW (MIG), SAW as precision layer-wound MIG spools (0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm) and straight cut-length TIG rods (1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm in 914mm / 36-inch and 1000mm lengths). Recommended shielding gas: 100% Argon (GTAW); Argon or Argon + Helium (GMAW).
Monel 400 filler wire offers unmatched durability in the splash and tidal zones of offshore oil & gas platforms, where alternating wet and dry aerated seawater rapidly corrodes steel. In refinery hydrofluoric (HF) acid alkylation units, ERNiCu-7 is the standard consumable for welding Monel 400 fractionator columns, valves and piping. Typical applications include: Offshore oil & gas platform riser and jacket splash-zone Monel 400 sheathing in the Arabian Gulf and North Sea; Refinery hydrofluoric (HF) acid alkylation columns, reboilers, valves and piping; Multi-Stage Flash (MSF) desalination brine heaters, demisters and vacuum salt evaporators.
International B2B Technical Enquiry & Quotation Request
Submit your alloy grade, AWS/ISO classification, diameter, welding process and delivery destination. Our technical export team in Mumbai responds to enquiries from the Middle East, GCC, USA, UK, Europe, Singapore, Sri Lanka, South Africa, Peru and global markets.