AWS A5.9 ER320 / ER320LR
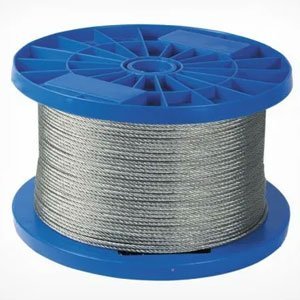
Alloy 20 Filler Wire
34Ni-20Cr-3.5Cu-2.5Mo-Nb wire (ER320/ER320LR) engineered to resist hot sulfuric acid, nitric-sulfuric mixtures and stress-corrosion cracking.
Specialized corrosion-resistant and high-temperature welding filler metals engineered for sulfuric acid plants, phosphoric acid evaporators, urea strippers, flue-gas scrubbers and dissimilar metal joints.
When standard 304L or 316L stainless steels suffer rapid general corrosion, stress-corrosion cracking or localized pitting, engineers specify high-alloy iron-nickel-chromium-molybdenum-copper or nickel-base consumables. FillerWires supplies specialized welding filler wires covering Alloy 20 (ER320 / ER320LR), super-austenitic grades (ER385 / 904L, ER383), urea-grade ER310MoL, high-ferrite dissimilar ER312, and severe-service Ni-Cr-Co-Mo and Ni-Mo-Cr alloys.
Contact us for confirmed product specifications and available technical documentation.
34Ni-20Cr-3.5Cu-2.5Mo-Nb wire (ER320/ER320LR) engineered to resist hot sulfuric acid, nitric-sulfuric mixtures and stress-corrosion cracking.
20Cr-25Ni-4.5Mo-1.5Cu low-carbon super-austenitic wire for welding UNS N08904 (904L) in phosphoric acid, sulfuric acid and seawater cooling equipment.
27Cr-31Ni-3.7Mo-1.0Cu ultra-low carbon filler wire for welding UNS N08028 heat exchangers in wet-process phosphoric acid concentration units.
Fully austenitic low-ferrite (≤0.5 FN) 25Cr-22Ni-2.2Mo filler wire designed for urea synthesis reactors, strippers and ammonium carbamate condensers.

ERNiCrMo-4 nickel-molybdenum-chromium filler wire for severe oxidizing/reducing chemical environments and FGD scrubber linings.

ERNiCrMo-10 filler wire offering exceptional resistance to oxidizing acid chlorides, wet chlorine and localized crevice corrosion.
ERNiCrCoMo-1 nickel-chromium-cobalt-molybdenum wire for extreme temperature petrochemical reformers and gas turbine ducting.
Titanium-deoxidized commercially pure nickel filler wire for molten caustic soda, chlor-alkali cell rooms and food-grade fatty acid processing.
Compare chemical compositions and primary corrosive or thermal media across our special alloy welding consumables. Contact us for confirmed product specifications and available technical documentation.
| Alloy Grade | AWS / ISO Standard | Nominal Composition (wt.%) | Primary Corrosive / Thermal Media |
|---|---|---|---|
| Alloy 20 (ER320 / ER320LR) | AWS A5.9 ER320LR | 34Ni – 20Cr – 3.5Cu – 2.5Mo – Nb (Low C, P, S, Si) | Hot sulfuric acid (20–40%), nitric-sulfuric mixtures, pickling tanks |
| ER385 (Alloy 904L) | AWS A5.9 ER385 / ISO 20 25 5 Cu L | 25Ni – 20Cr – 4.5Mo – 1.5Cu – ≤0.025C | Phosphoric acid, dilute sulfuric acid, chloride cooling water |
| ER383 (Alloy 28) | AWS A5.9 ER383 / ISO 27 31 4 Cu L | 31Ni – 27Cr – 3.7Mo – 1.0Cu – ≤0.025C | Concentrated wet-process phosphoric acid evaporators & sour gas |
| ER310MoL | EN ISO 14343 25 22 2 N L | 25Cr – 22Ni – 2.2Mo – 0.14N – ≤0.02C | High-pressure urea strippers & ammonium carbamate condensers |
| ER312 | AWS A5.9 ER312 | 29Cr – 9Ni (High Delta-Ferrite ~40 FN) | Dissimilar high-carbon/tool steels, abrasion buffer layers, shaft repair |
| Hastelloy C276 | AWS A5.14 ERNiCrMo-4 | 57Ni – 16Mo – 15.5Cr – 3.8W – 5.5Fe | Wet chlorine, ferric/cupric chlorides, hot contaminated mineral acids |
| Inconel 617 | AWS A5.14 ERNiCrCoMo-1 | 52Ni – 22Cr – 12.5Co – 9Mo – 1.2Al | Carburizing, nitriding & oxidizing atmospheres up to 1100°C |
| Pure Nickel (ERNi-1) | AWS A5.14 ERNi-1 | ≥93Ni – 2.0–3.5Ti | Concentrated caustic soda (NaOH), dry chlorine & halogens |
Chemical complexes, fertilizer plants, mining autoclaves and refineries across the following international destinations source special alloy welding wires:
| Target Country | Relevant Industrial Cities & Chemical Hubs | Primary Special Alloy Grades in Demand |
|---|---|---|
| Saudi Arabia & UAE | Jubail, Yanbu, Ras Al-Khair, Dammam, Abu Dhabi, Ruwais, Dubai, Jebel Ali | Alloy 20 (ER320LR), ER385 (904L), ER383, ER310MoL for phosphate, urea & acid plants |
| Oman, Qatar, Kuwait & Bahrain | Sohar, Muscat, Duqm, Salalah, Mesaieed, Ras Laffan, Ahmadi, Shuaiba, Sitra | Inconel 617, Hastelloy C276, ER310MoL, ER312 for fertilizer & refining units |
| United States & United Kingdom | Houston, Baton Rouge/New Orleans, Pittsburgh, Chicago, Sheffield, Birmingham, Billingham/Newcastle | Alloy 20, Hastelloy C22/C276, Inconel 617, Pure Nickel ERNi-1 |
| Germany, Italy, Belgium & Netherlands | Frankfurt, Ludwigshafen/Mannheim, Hamburg, Milan, Turin, Antwerp, Rotterdam | EN ISO / AWS certified ER385, ER383, ER320LR, ERNiCrMo-10 (C22) |
| South Africa, Peru, Singapore & Sri Lanka | Johannesburg, Durban, Richards Bay, Rustenburg, Lima, Callao, Arequipa, Jurong, Colombo | Alloy 20, ER385 (904L) & Hastelloy C276 for sulfuric acid leaching & chemical plants |
Technical guidance on Alloy 20, ER385 (904L), ER383, ER310MoL and ER312 welding consumables.
Because Alloy 20 (34Ni-20Cr-3.5Cu-2.5Mo-Nb) solidifies as 100% austenite with zero delta-ferrite, AWS A5.9 ER320LR restricts carbon, silicon, phosphorus and sulfur to ultra-low levels to prevent hot microfissuring during multi-pass GTAW and GMAW welding in sulfuric acid service.
Wet-process phosphoric acid evaporators utilize super-austenitic ER385 (Alloy 904L) and ER383 (Alloy 28), whereas high-pressure urea synthesis strippers and carbamate condensers require ultra-low ferrite ER310MoL (25Cr-22Ni-2Mo) filler wire.
ER312 (~29Cr-9Ni) deposits a high-ferrite (~40 FN) austenitic-ferritic weld metal with exceptional tolerance for dilution and high resistance to hot cracking when welding hard-to-weld steels, high-carbon steels, tool steels and dissimilar maintenance joints.