Inconel 625 Filler Wire Supplier — AWS A5.14 ERNiCrMo-3 Welding Wire
High-strength Nickel-Chromium-Molybdenum-Niobium filler metal (AWS A5.14 ERNiCrMo-3 / UNS N06625) for offshore sour-gas weld overlay cladding, super-austenitic stainless welding and cryogenic-to-980°C service.
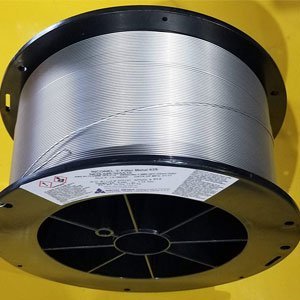
Industry-Standard ERNiCrMo-3 Filler Metal for Sour Service Cladding & High-Alloy Joining
Inconel 625 Filler Wire (AWS A5.14 ERNiCrMo-3 / Alloy 625 Filler Metal) is one of the most widely specified nickel-base welding consumables in international oil & gas, marine, chemical and power engineering. Its solid-solution matrix of nickel (~61%), chromium (21.5%), molybdenum (9%) and niobium (3.6%) delivers exceptional tensile strength and fatigue resistance from cryogenic temperatures (-196°C) up to 980°C without requiring precipitation heat treatment.
With a Pitting Resistance Equivalent Number (PREN = %Cr + 3.3×%Mo + 16×%N) exceeding 50, ERNiCrMo-3 is the benchmark consumable for automated GTAW/GMAW corrosion-resistant weld overlay (CRA cladding) on carbon and low-alloy steel subsea Christmas trees, valves, risers and pressure vessels, as well as over-matching welds on 6% Mo super-austenitic stainless steels (such as 254 SMO / UNS S31254 and AL-6XN).
Alloy Identification, Standards & Supply Specifications
Niobium and molybdenum stiffen the nickel-chromium matrix directly in the as-welded state while providing outstanding resistance to chloride pitting, crevice corrosion and H2S/CO2 sour-gas stress-corrosion cracking.
| Product Designation | Inconel 625 Filler Wire (TIG Welding Rod / MIG Spooled Wire) |
|---|---|
| AWS / ASME Classification | AWS A5.14 ERNiCrMo-3 |
| EN / ISO Classification | EN ISO 18274 S Ni 6625 (NiCr22Mo9Nb) |
| UNS Designation & Werkstoff Nr. | UNS N06625 • W.Nr. 2.4856 / 2.4831 |
| Compatible Base Materials | Alloy 625 (UNS N06625), Alloy 825 (UNS N08825), 6% Mo super-austenitic stainless steels (UNS S31254, N08367, N08926), 9% Ni cryogenic steels, and dissimilar joints or CRA overlays onto carbon/low-alloy steels (AISI 4130, F22, X65). |
| Supported Welding Processes | GTAW (TIG), GMAW (MIG / Pulsed), SAW, Hot-Wire TIG Cladding |
| Shielding Gas Recommendations | 100% Argon or Ar + He (GTAW); Ar + 25–30% He (Pulsed GMAW) |
| Available Wire Diameters | MIG Spools: 0.8mm (.030"), 0.9mm (.035"), 1.0mm (.040"), 1.2mm (.045"), 1.6mm (1/16") TIG Cut-Length Rods: 1.2mm, 1.6mm (1/16"), 2.0mm, 2.4mm (3/32"), 3.2mm (1/8"), 4.0mm (5/32") × 914mm (36") / 1000mm |
| Packaging & Storage | TIG Rods: 5 kg / 10 kg moisture-resistant tubular plastic packs in export master cartons. MIG Wire: 12.5 kg / 15 kg precision layer-wound BS300 / S200 spools sealed in VCI polyethylene film. Storage: Store in a dry, temperature-controlled indoor store (+10°C to +40°C, <60% RH) in original sealed packaging. |
Chemical Composition Specification (AWS A5.14 ERNiCrMo-3)
The table below specifies the standard wire chemical composition limits in weight percent (wt.%). Single values represent maximum permissible limits unless stated otherwise:
| Element | Verified Specification Limit (wt.%) | Metallurgical Function in Weld Metal |
|---|---|---|
| Nickel (Ni) | 58.0 min (Typical: 61–64) | Austenitic matrix immune to chloride stress-corrosion cracking |
| Chromium (Cr) | 20.0 – 23.0 | Passivation against oxidizing media and high-temperature sulfidation |
| Molybdenum (Mo) | 8.0 – 10.0 | High resistance to localized chloride pitting and crevice attack |
| Niobium + Tantalum (Nb+Ta) | 3.15 – 4.15 | Solid-solution strengthening and stabilization against sensitization |
| Iron (Fe) | 5.0 max (Often <1.0% for low-dilution overlays) | Controlled low iron supports single/two-layer CRA cladding compliance |
| Carbon (C) | 0.10 max (Typical: ≤0.03) | Low carbon maintains ductility and intergranular corrosion resistance |
| Manganese (Mn) | 0.50 max | Deoxidation and sulfur control |
| Silicon (Si) | 0.50 max | Restricted to prevent silicate film formation and microfissuring |
| Aluminum (Al) & Titanium (Ti) | Al ≤ 0.40, Ti ≤ 0.40 | Deoxidizers |
| Phosphorus (P) & Sulfur (S) | P ≤ 0.020, S ≤ 0.015 | Strict impurity limits for crack-free multi-pass welds |
Mechanical & Physical Properties
The values below distinguish between minimum AWS/ISO classification requirements for all-weld-metal test assemblies and typical as-welded deposited weld metal benchmarks:
| Property | Value | Unit | Specification / Reference Basis |
|---|---|---|---|
| Tensile Strength | ≥ 760 (Typical: 785 – 830) | MPa | AWS A5.14 Minimum / Typical All-Weld-Metal |
| Yield Strength (0.2% Offset) | ≥ 450 (Typical: 480 – 540) | MPa | Typical As-Welded GTAW/GMAW Deposit |
| Elongation | ≥ 30 (Typical: 34 – 40) | % | AWS A5.14 Minimum in 4D |
| Charpy V-Notch Impact (-196°C) | ≥ 70 | J | Typical Cryogenic Weld Metal Toughness |
| Density | 8.44 | g/cm³ | Physical Property Reference |
| Melting Range | 1290 – 1350 | °C | Physical Property Reference |
Corrosion Resistance, Welding Considerations & Industrial Applications
Inconel 625 filler wire resists seawater pitting, stagnant marine crevice attack, sour gas (H2S + chlorides + elemental sulfur), nitric-hydrofluoric pickling solutions and flue gas condensates. When cladding carbon steel (e.g., API 6A / NACE MR0175 / ISO 15156 applications where <5% or <10% Fe is required at the finished overlay surface), control arc energy and overlap step-over to limit base metal iron dilution.
Typical Industrial Applications
- Automated GTAW (hot-wire TIG) and pulsed GMAW CRA weld overlay cladding of oil & gas valves, flanges, subsea manifolds and risers
- Welding 6% Mo super-austenitic stainless steel desalination high-pressure SWRO piping and seawater cooling networks
- Joining 9% Nickel cryogenic LNG storage tanks and liquefied gas transfer lines
- Offshore exhaust systems, flare tips, bellows expansion joints and marine propellers
- Dissimilar welding between nickel alloys, stainless steels and carbon/low-alloy steels
International Enquiry Destinations
FillerWires welcomes B2B export enquiries for Inconel 625 Filler Wire from EPC contractors, process equipment fabricators, shipyards and distributors across the following priority countries and industrial cities:
| Target Country | Relevant Industrial Cities & Ports | Typical Regional Sector Demand |
|---|---|---|
| United Arab Emirates | Abu Dhabi, Dubai, Jebel Ali, Sharjah, Fujairah | Offshore oilfield CRA weld overlay cladding & shipyards |
| Saudi Arabia | Dammam, Jubail, Khobar, Dhahran, Yanbu | Sour gas manifold cladding, refining & desalination |
| Qatar | Doha, Ras Laffan, Mesaieed | LNG cryogenic piping & offshore North Field platforms |
| Oman, Kuwait & Bahrain | Muscat, Sohar, Duqm, Ahmadi, Shuaiba, Manama, Hidd | Refinery vessels, wellhead cladding & seawater piping |
| United States & United Kingdom | Houston, New Orleans, Pittsburgh, Aberdeen, Sheffield, Glasgow | Subsea trees, blowout preventers & North Sea offshore |
| Norway, Italy & Germany | Stavanger, Bergen, Milan, Genoa, Hamburg, Düsseldorf | Subsea engineering, pressure vessels & heat exchangers |
| Singapore, South Africa & Peru | Jurong, Tuas, Pioneer, Johannesburg, Durban, Lima, Callao | FPSO topside modules & chemical processing |
Frequently Asked Questions — Inconel 625 Filler Wire
Technical questions and answers regarding classification, base metal compatibility, welding parameters and procurement for Inconel 625 Filler Wire:
Inconel 625 Filler Wire is classified under AWS A5.14 ERNiCrMo-3 and EN ISO 18274 S Ni 6625 (NiCr22Mo9Nb) (UNS UNS N06625, Werkstoff Nr. 2.4856 / 2.4831). Contact us for confirmed product specifications and available technical documentation.
Inconel 625 Filler Wire (AWS A5.14 ERNiCrMo-3) is engineered for welding Alloy 625 (UNS N06625), Alloy 825 (UNS N08825), 6% Mo super-austenitic stainless steels (UNS S31254, N08367, N08926), 9% Ni cryogenic steels, and dissimilar joints or CRA overlays onto carbon/low-alloy steels (AISI 4130, F22, X65).
Inconel 625 Filler Wire is supplied for GTAW (TIG), GMAW (MIG / Pulsed), SAW, Hot-Wire TIG Cladding as precision layer-wound MIG spools (0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm) and straight cut-length TIG rods (1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm in 914mm / 36-inch and 1000mm lengths). Recommended shielding gas: 100% Argon or Ar + He (GTAW); Ar + 25–30% He (Pulsed GMAW).
Inconel 625 filler wire resists seawater pitting, stagnant marine crevice attack, sour gas (H2S + chlorides + elemental sulfur), nitric-hydrofluoric pickling solutions and flue gas condensates. When cladding carbon steel (e.g., API 6A / NACE MR0175 / ISO 15156 applications where <5% or <10% Fe is required at the finished overlay surface), control arc energy and overlap step-over to limit base metal iron dilution. Typical applications include: Automated GTAW (hot-wire TIG) and pulsed GMAW CRA weld overlay cladding of oil & gas valves, flanges, subsea manifolds and risers; Welding 6% Mo super-austenitic stainless steel desalination high-pressure SWRO piping and seawater cooling networks; Joining 9% Nickel cryogenic LNG storage tanks and liquefied gas transfer lines.
International B2B Technical Enquiry & Quotation Request
Submit your alloy grade, AWS/ISO classification, diameter, welding process and delivery destination. Our technical export team in Mumbai responds to enquiries from the Middle East, GCC, USA, UK, Europe, Singapore, Sri Lanka, South Africa, Peru and global markets.